6x19 vs 6x37 Wire Rope — Differences and Selection Guide
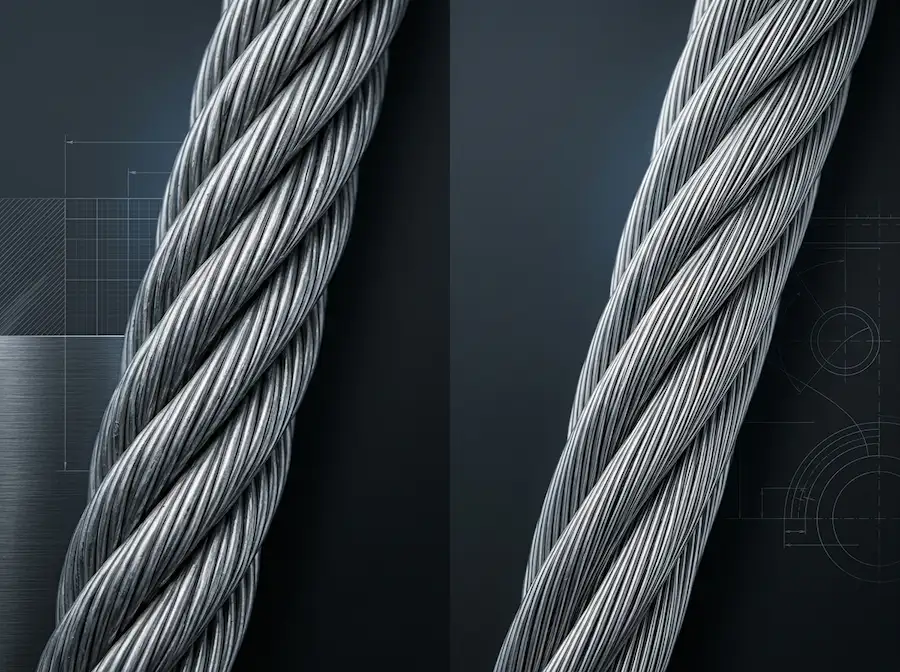
Side-by-side comparison of 6x19 and 6x37 wire rope constructions — wire arrangement, flexibility, abrasion resistance, fatigue performance and selection guidance for industrial lifting.
This article provides general technical reference. Wire rope construction, diameter, core and finish selection should be verified against the applicable product standard, design factor, equipment specification and service environment.
Two construction designations dominate six-strand steel wire rope procurement: 6×19 and 6×37. Both share the same overall architecture — six strands laid helically around a central core — and both are defined under ISO 2408, ASTM A1023/A1023M and EN 12385. The single defining difference is the number and diameter of the individual wires inside each strand.
That difference has a direct effect on the four performance characteristics that drive rope life: flexibility, abrasion resistance, fatigue performance and crushing resistance. Selecting between 6×19 and 6×37 is therefore not a question of “better” or “worse” — it is a question of which trade-off best matches the operating conditions of the equipment.
This article compares the two constructions in detail and provides a selection framework for the most common industrial applications.
Reading a Wire Rope Designation
Wire rope construction is described by the notation a × b, where a is the number of outer strands and b is the approximate number of wires in each strand. For six-strand ropes covered in this comparison:
| Designation | Outer strands | Wires per strand (approx.) | Strand family |
|---|---|---|---|
| 6×7 | 6 | 7 | Coarse (extra-rugged) |
| 6×19 | 6 | 19 | General purpose |
| 6×37 | 6 | 37 | Flexible |
| 8×19 / 8×25 | 8 | 19 – 25 | Specialty / elevator |
Within the 6×19 and 6×37 families, individual strand constructions are typically specified by name — Seale, Warrington, Filler or a combination — which describe how the wires pack inside the strand. These variants modify the flexibility/abrasion balance further, but the overall designation (6×19 or 6×37) remains the primary parameter.
For the purpose of selection, two questions matter:
- How many bending cycles will the rope experience during its service life?
- Will the rope see surface abrasion from external contact?
The answer to these two questions almost always determines whether 6×19 or 6×37 is the right starting point.
6×19 Wire Rope
Construction
A 6×19 wire rope contains six strands, each built from approximately 19 wires. The strand typically includes a mixture of larger and smaller wires arranged in a Seale, Warrington or Filler pattern. Because the strand contains fewer wires than a 6×37 strand, each individual wire has a larger diameter for the same overall rope diameter.
The larger individual wire diameter is the source of the construction’s main advantages — and its main limitations.
Characteristics
| Property | Rating | Practical meaning |
|---|---|---|
| Flexibility | Moderate | Acceptable for standard crane sheaves and drums |
| Abrasion resistance | High | Outer wires carry more material per surface contact |
| Fatigue (bending) life | Moderate | Each wire takes a larger share of the bending strain |
| Crushing resistance | Good | Larger wires resist flattening under lateral load |
| Structural stability | High | Less tendency to birdcage or unlay under shock load |
Typical Applications
6×19 is the workhorse of general industrial wire rope. It is commonly selected for:
- Overhead and gantry cranes in factories and shipyards
- Construction hoists and material-handling equipment
- Winch lines on mobile equipment
- Slings and rigging in heavy lift operations
- General-purpose industrial applications where bending cycles are moderate
In environments where the rope is exposed to grit, sand or rough surfaces (quarries, construction sites, foundry charging), the larger outer wires of a 6×19 construction tend to outlast a 6×37 rope of the same diameter.
6×37 Wire Rope
Construction
A 6×37 wire rope contains six strands, each built from approximately 37 wires. The additional wires are accommodated by using finer wire diameters and a more complex strand layout — typically a Seale-on-Seale, Warrington-Seale or Filler construction.
The finer wires and more complex strand geometry give the rope noticeably more flexibility than a 6×19 construction of equivalent diameter.
Characteristics
| Property | Rating | Practical meaning |
|---|---|---|
| Flexibility | High | Bends easily around smaller sheaves and multi-sheave blocks |
| Abrasion resistance | Moderate | Outer wires wear through faster under surface contact |
| Fatigue (bending) life | High | Smaller wires distribute bending strain across more filaments |
| Crushing resistance | Moderate | Smaller wires can flatten more easily under side load |
| Structural stability | Good | Stable in service but less tolerant of shock loads than 6×19 |
Typical Applications
6×37 is preferred where the rope must bend frequently or wrap around smaller sheaves. Common applications include:
- Mobile and crawler crane hoist ropes
- Elevator and lift traction ropes (specialised 8-strand variants descend from the 6×37 family)
- Crane reeving systems with multiple sheaves
- Mechanical power transmission and control cables
- Hoists where the rope operates over small diameter drums
In continuous-duty applications where the rope passes over sheaves thousands of times per day, the higher fatigue life of 6×37 typically outlasts 6×19, even when the 6×19 rope offers higher per-cycle abrasion resistance.
Side-by-Side Comparison
The table below summarises the practical trade-offs between the two constructions for engineering and procurement purposes.
| Parameter | 6×19 wire rope | 6×37 wire rope |
|---|---|---|
| Wires per strand | ~19 (fewer, larger) | ~37 (more, smaller) |
| Strand family | General purpose | Flexible |
| Flexibility | Moderate | High |
| Abrasion resistance | Higher | Lower |
| Fatigue (bending) life | Moderate | Higher |
| Crushing resistance | Higher | Lower |
| Shock-load tolerance | Higher | Lower |
| Minimum sheave D/d ratio | ~20 : 1 (general lifting) | ~16 – 18 : 1 (smaller sheaves OK) |
| Typical rope grades | 1570 – 1960 MPa | 1570 – 1960 MPa |
| Typical MBL construction factor (K) | ≈ 0.33 (6×19 class average) | ≈ 0.29 (6×37 class average) |
| Suitable environment | Outdoor, abrasive, moderate cycles | Indoor, frequent cycles, clean |
| Typical industries | Construction, mining, shipyards, mobile equipment | Elevators, mobile cranes, mechanical drive, control systems |
Two practical observations follow from this comparison:
- The two constructions are not substitutes in the same duty cycle. A 6×19 rope in a high-cycle application will fail by fatigue; a 6×37 rope in an abrasive environment will fail by surface wear.
- Where duty is genuinely mixed, design factor and inspection frequency matter more than the basic construction choice.
Selection Framework
The selection between 6×19 and 6×37 is governed by four operating parameters:
1. Bending Cycles and Sheave Diameter
For high-cycle applications or equipment with small sheaves or drums, the 6×37 construction provides a meaningful fatigue-life advantage. The required minimum sheave diameter (D/d ratio) is also lower, allowing more compact equipment designs.
2. Surface Abrasion and External Wear
For environments where the rope contacts abrasive surfaces — sand, grit, slag, concrete, rough structures — 6×19 typically lasts longer. The larger outer wires provide more wear material before failure criteria are reached.
3. Shock Loading and Side Pressure
For applications involving shock loads, side loading or risk of crushing (e.g. multi-layer drum spooling, slack rope conditions, fishing and trawling), 6×19 is generally more tolerant because of its larger wires and stiffer strand construction.
4. Cost and Availability
6×19 is typically less expensive and more widely available in commodity sizes and grades. 6×37, particularly in higher tensile grades, may carry a premium and longer lead time in some markets. For standard crane duty on a fixed budget, 6×19 is often the default.
Decision Summary
| Operating condition | Recommended construction |
|---|---|
| High bending cycles, small sheaves, clean environment | 6×37 |
| Abrasive environment, moderate cycles, outdoor service | 6×19 |
| Mixed industrial lifting, standard crane duty | 6×19 (default) |
| Elevator or lift traction ropes | 6×37 / 8×19 / 8×25 |
| Mobile crane hoist ropes (high cycle count) | 6×37 |
| Winch and general rigging | 6×19 |
| Shock-loaded or multi-layer drum spooling | 6×19 |
| Mechanical power transmission (control cables, drives) | 6×37 |
Factors Beyond Construction Type
Construction is the dominant selection parameter, but four further choices significantly affect rope performance and life.
Rope Diameter
Larger diameter increases breaking strength (MBL scales approximately with d²), reduces wear per unit load and extends service life. Equipment compatibility sets the practical ceiling — drum width, sheave groove dimensions, end fitting geometry and structural weight all constrain diameter selection. Undersized ropes fail by overstress; oversized ropes add cost and weight without proportional benefit.
Core Type
The core determines internal stability and temperature resistance.
- Fibre core (FC) — natural or synthetic fibre. Provides the highest flexibility and acts as a lubricant reservoir. Used in general-purpose rope where temperature limits are acceptable.
- Independent wire rope core (IWRC) — a separate wire rope used as the core. Provides higher strength, better heat resistance and higher crushing resistance. Standard for crane duty and high-temperature service.
- Wire strand core (WSC) — a single steel strand at the centre. Sits between FC and IWRC in performance.
For most crane and rigging applications, IWRC is preferred. For applications where maximum flexibility is needed and operating temperatures are moderate, fibre core may be specified.
Surface Finish
The finish determines corrosion performance and, to a lesser extent, fatigue behaviour.
| Service environment | Recommended finish |
|---|---|
| Indoor, dry, controlled | Bright (ungalvanized) carbon steel |
| Outdoor, industrial atmosphere | Galvanized, Class A or Class B per ASTM A741 1 |
| Marine immersion, chemical, food-grade | Stainless steel 304 / 316 |
Galvanizing slightly reduces fatigue life compared with bright wire, because the zinc coating introduces micro-notches on the wire surface. In corrosive environments, this trade-off is almost always favourable because the alternative is rapid loss of cross-section by rust.
Tensile Grade
Wire rope is supplied in standardized tensile grades (rope grades), typically 1370, 1570, 1770, 1960 and 2160 MPa. Higher grades provide more strength per unit diameter but are less tolerant of shock loads and nicks. For general lifting, 1770 or 1960 MPa is the most common range.
Specification and Procurement
A complete wire rope specification for procurement should include the following items:
- Construction — 6×19 (with strand type) or 6×37 (with strand type).
- Nominal diameter — in millimetres.
- Rope grade — wire tensile strength (e.g. 1960 MPa).
- Core type — FC, IWRC or WSC.
- Lay pattern — right regular lay is the default; lang lay for specific applications.
- Finish — bright, galvanized or stainless.
- Material — carbon steel (standard) or stainless steel grade (304 / 316).
- Minimum breaking load (MBL) — calculated or specified.
- Length and reel format — cut length or full drum.
- End fittings — none (for socketing on receipt), spliced eye, swaged socket or wedge socket.
- Applicable standard — ISO 2408 2, ASTM A1023/A1023M 3, EN 12385 4 or equivalent.
- Inspection and replacement criteria — typically per ISO 4309 5 for crane duty.
For international projects, the supplied rope is usually marked with the manufacturer’s identification, the construction designation, the rope grade and the standard of manufacture. Verifying these markings against the purchase specification on receipt is a standard part of incoming inspection.
Conclusion
The choice between 6×19 and 6×37 wire rope is fundamentally a trade-off between abrasion resistance and flexibility. 6×19 is the more rugged construction — larger wires, higher surface durability, better behaviour under shock and side load. 6×37 is the more flexible construction — more wires, better fatigue life, smaller minimum sheave diameter.
For applications dominated by bending cycles (mobile crane hoist ropes, elevator traction ropes, control cables), 6×37 is the appropriate starting point. For applications dominated by surface wear, shock loads and rugged duty (construction cranes, mining, shipyards, outdoor rigging), 6×19 is generally the more cost-effective choice.
A complete specification combines the construction choice with the appropriate core, finish, tensile grade and end fittings. The standards — ISO 2408, ASTM A1023/A1023M and EN 12385 — provide the engineering data and the common language for specifying each parameter.
For the broader context on wire rope construction, lay pattern and finish selection, see Steel Wire Rope Explained — Construction, Types, Grades and Applications.
References
-
ASTM International, ASTM A741/A741M — Standard Specification for Metallic-Coated Steel Wire Rope and Fittings for Highway Guardrail. ASTM A741 ↩
-
International Organization for Standardization, ISO 2408:2017 — Steel wire ropes for general purposes — Requirements. ISO 2408 ↩
-
ASTM International, ASTM A1023/A1023M — Standard Specification for Stranded Carbon Steel Wire Ropes for General Purposes. ASTM A1023 ↩
-
European Committee for Standardization, EN 12385 (series) — Steel wire ropes — Safety. EN 12385 ↩
-
International Organization for Standardization, ISO 4309:2017 — Cranes — Wire ropes — Care and maintenance, inspection and discard. ISO 4309 ↩
Citar como Wayland Steel Editorial Team (2026). 6x19 vs 6x37 Wire Rope — Differences and Selection Guide. Wayland Steel Insights. https://www.waylandsteel.com.cn/es-es/insights/6x19-vs-6x37-wire-rope-differences-selection-guide/
¿Necesita una Solución Metálica Industrial?
Wayland Steel ofrece productos de acero, aleaciones de cobre y soluciones de aluminio para aplicaciones industriales globales.